 To be the most satisfactory energy and environment company in the world


Focus on global challenges and pressures, provide competitive energy and environmental solutions and services, and continuously create maximum value for customers.
Technical Characteristics

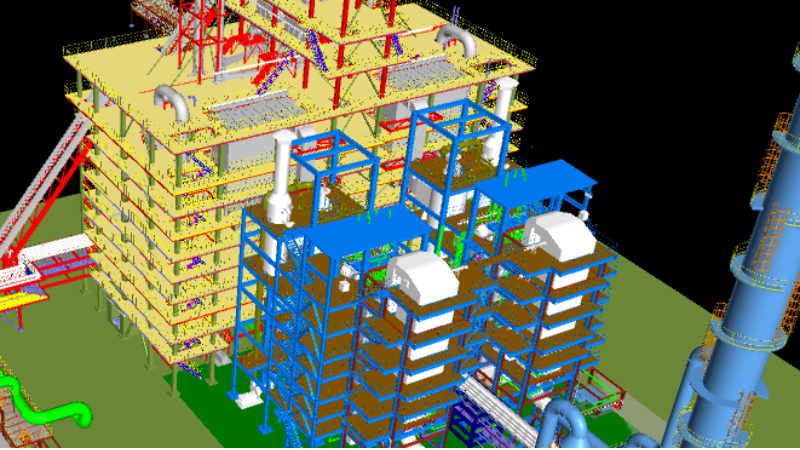
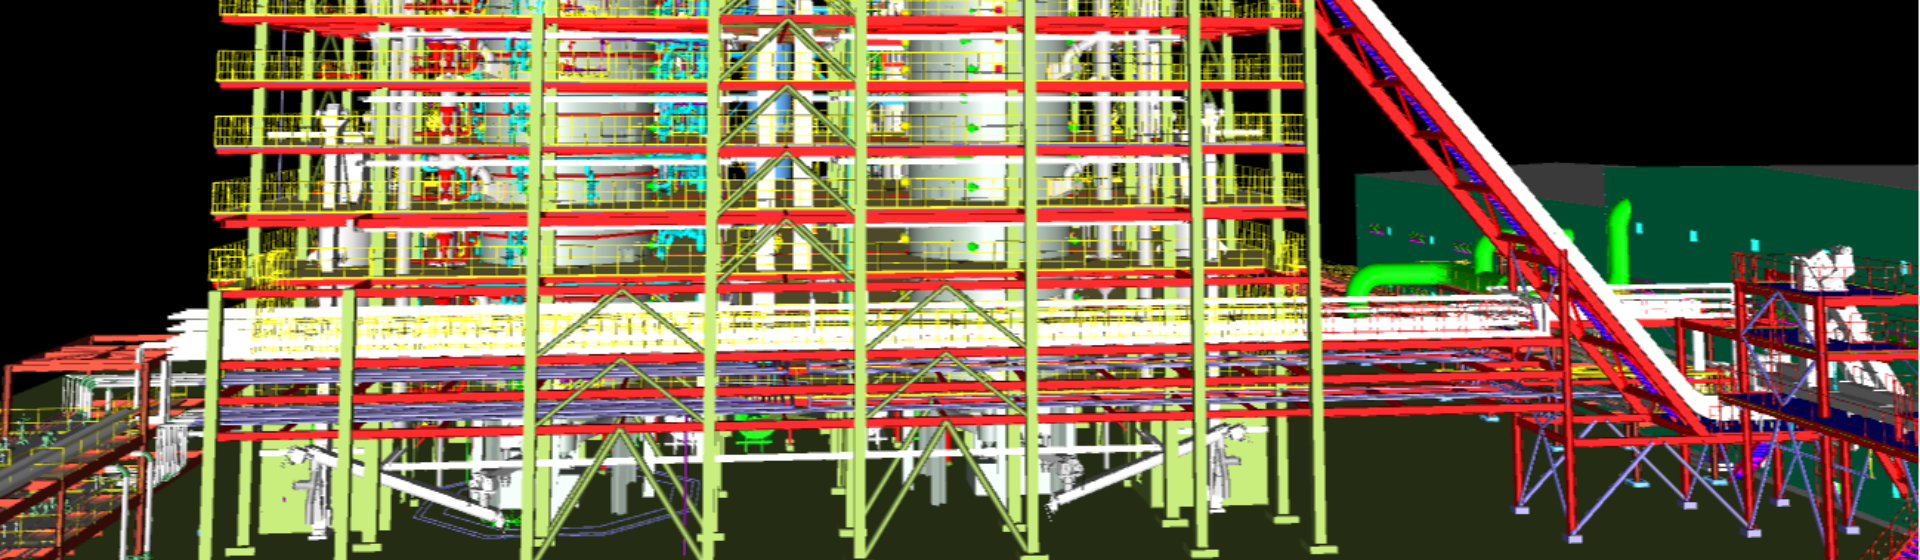
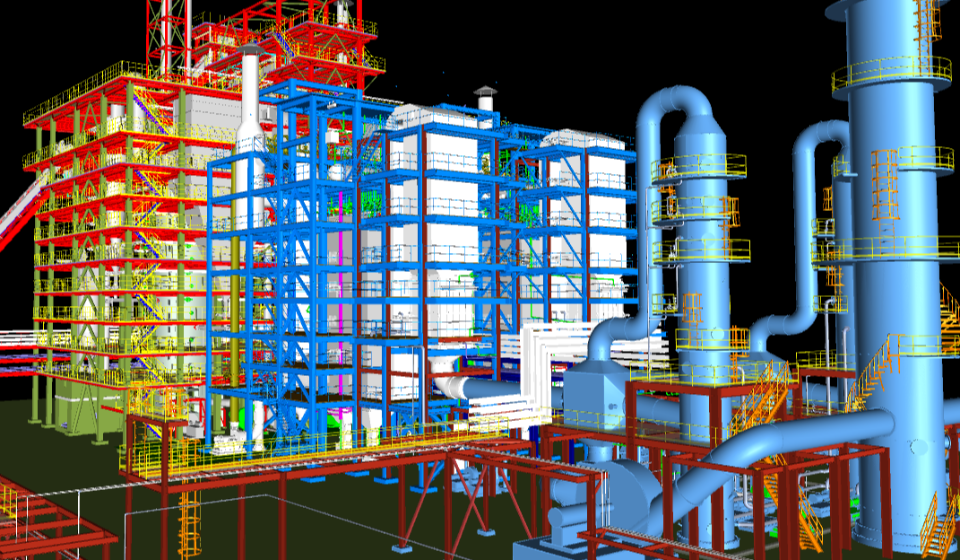
The unit includes the MHF and refractory, burners, cyclone separator, metal-membrane dust collector, CO burnout chamber, waste-heat boiler, denitrification system, structural steel frame, reducing-agent dosing, induced- and forced-draft fans, ducts, stack, CEMS, power supply and controls. Environmental facilities meet GB 18484 requirements. The MHF accommodates complex and unpredictable filter-cake composition and maintains stable combustion when moisture and composition fluctuate. Equipment and piping materials are selected for the corrosiveness of the process streams. Precise temperature and atmosphere control enriches valuable metals, with recovery described in the source as well above the industry average.
Solution

A specially designed feeding system with storage hoppers, scraper conveyors and screw conveyors reduces plugging and chain failure and delivers wet cake reliably to the furnace feed hopper. A cyclone and metal-membrane dust collector at the furnace outlet control entrained particulate matter to ≤10 mg/Nm³. A complete bottom-ash handling train, including a water-cooled screw conveyor, bucket elevator, metal-ash silo and bulk-bag packing machine, recovers valuable metals for resource utilization. The independently designed integrated process provides strong system compatibility and long-term stable operation.
Get The Effect
Annual filter-cake treatment is 60,000 tonnes. At an assumed off-site hazardous-waste disposal cost of RMB 2,000 per tonne, avoided disposal costs are RMB 120 million annually. Two 18.5 t/h waste-heat boilers generate estimated annual steam revenue of RMB 59.2 million at RMB 200 per tonne of steam. Design emissions outperform GB 18484: SO₂ ≤30 mg/Nm³, HCl ≤50 mg/Nm³, HF ≤1 mg/Nm³, dust ≤10 mg/Nm³ and NOx ≤40 mg/Nm³.