 To be the most satisfactory energy and environment company in the world


Focus on global challenges and pressures, provide competitive energy and environmental solutions and services, and continuously create maximum value for customers.
Technical Characteristics

Self-sustaining operation uses the concentrate's high calorific value as the main fuel, with natural gas for auxiliary firing, startup and shutdown. Rated steam output per furnace is at least 40 t/h. The operating range is 30–120%, accommodating production fluctuations. Feedwater temperatures of either 190°C or 260°C are accommodated by adjusting natural-gas consumption while maintaining rated steam output.
Solution

A pre-combustion chamber and low-NOx burners ensure complete destruction of organics, with specific organic pollutants and non-methane hydrocarbons meeting GB 31571-2015 and Beijing local standard DB11/447-2015.
Flue gas is treated by a bag filter using PTFE bags with PTFE membranes, followed by SNCR denitrification and stack CEMS monitoring. Outlet dust is guaranteed at ≤5 mg/Nm³.
Project-specific requirements and both cited standards apply simultaneously. Guaranteed limits are particulate matter ≤5 mg/Nm³, NOx ≤35 mg/Nm³, SO₂ ≤35 mg/Nm³, non-methane hydrocarbons (VOCs) ≤20 mg/Nm³ and dioxins ≤0.1 ng-TEQ/Nm³, supporting first-pass environmental acceptance.
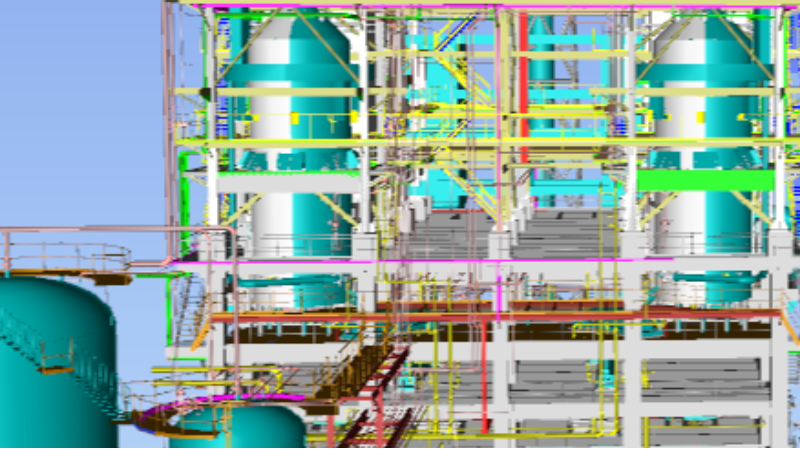
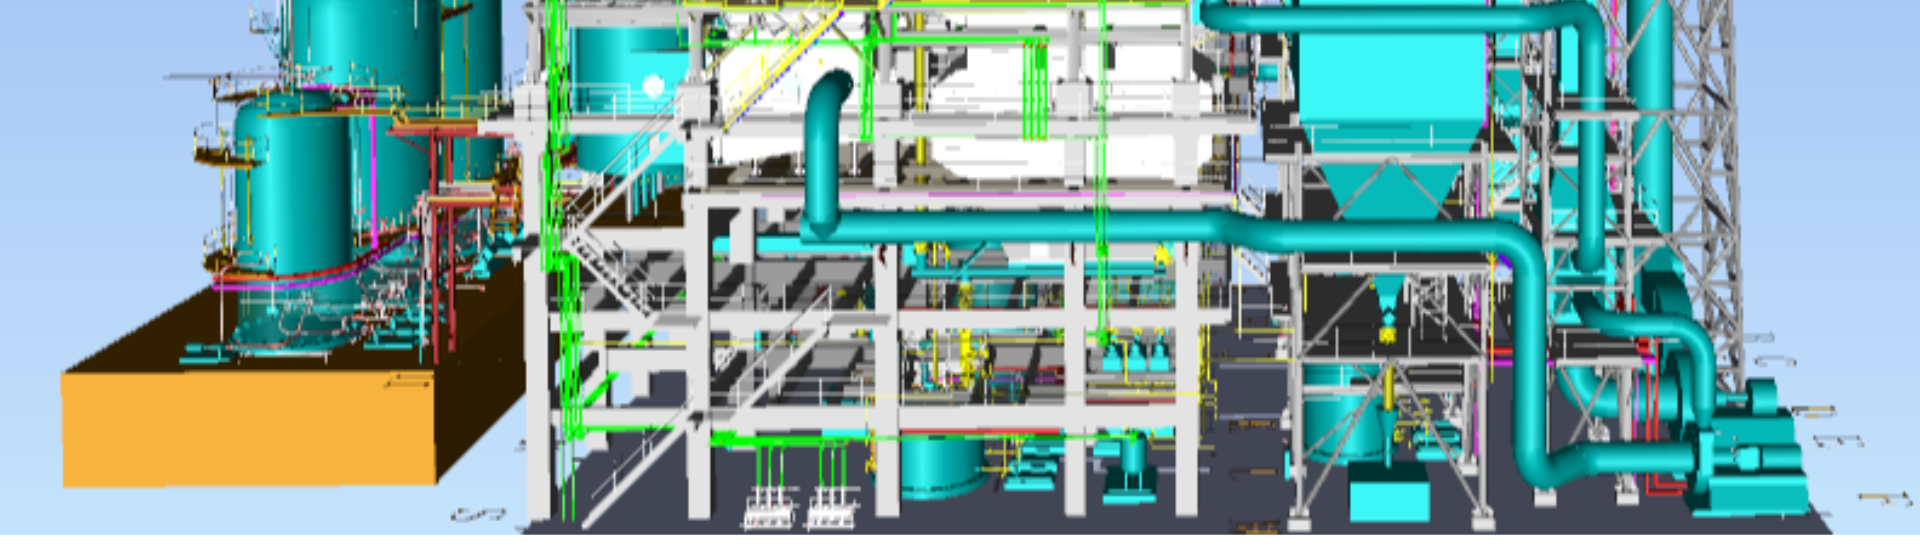
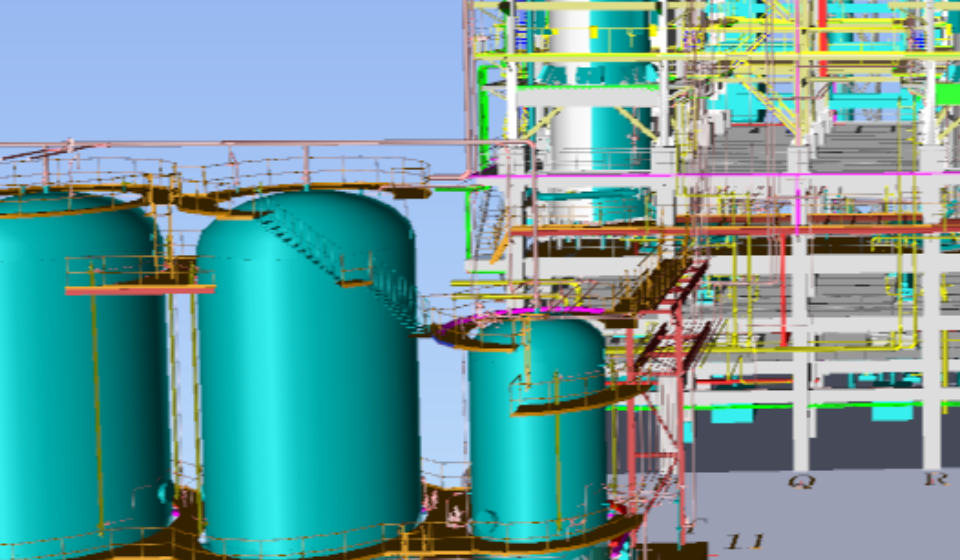
Get The Effect
Per-furnace capacity is 10 t/h of concentrate at 50–70% solids. Design operating range is 30–120%. Steam output is at least 40 t/h at 9.8 MPa(g) and 330°C. Guaranteed boiler efficiency on a lower-heating-value basis is at least 83.8%.